EN
 RU
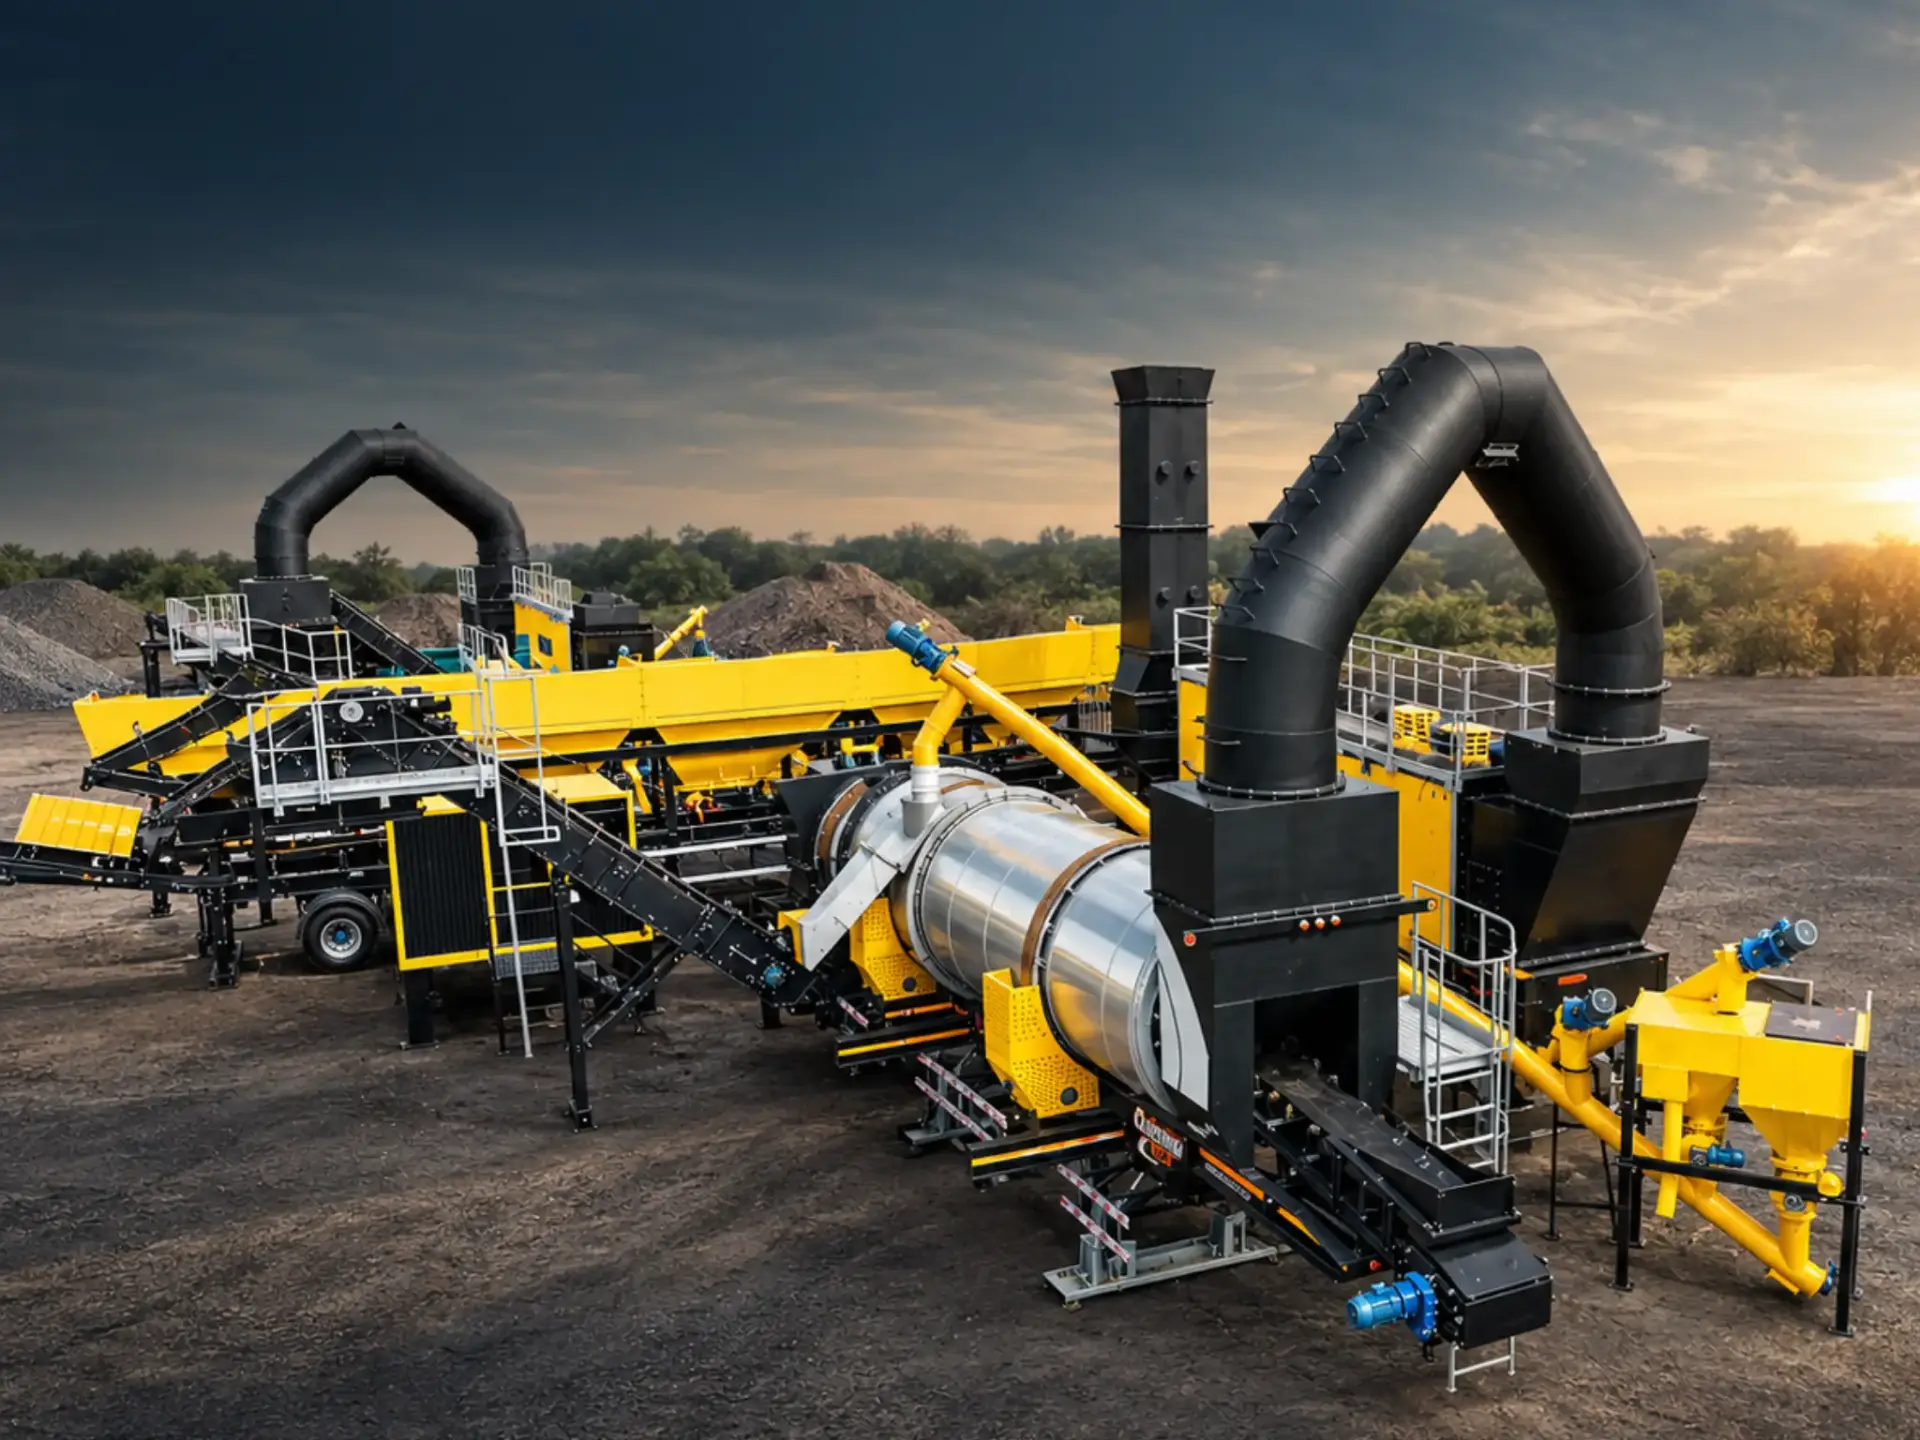
QUICKMIX | Mobile Counter Flow Drum Mix Plant (90-200 TPH)
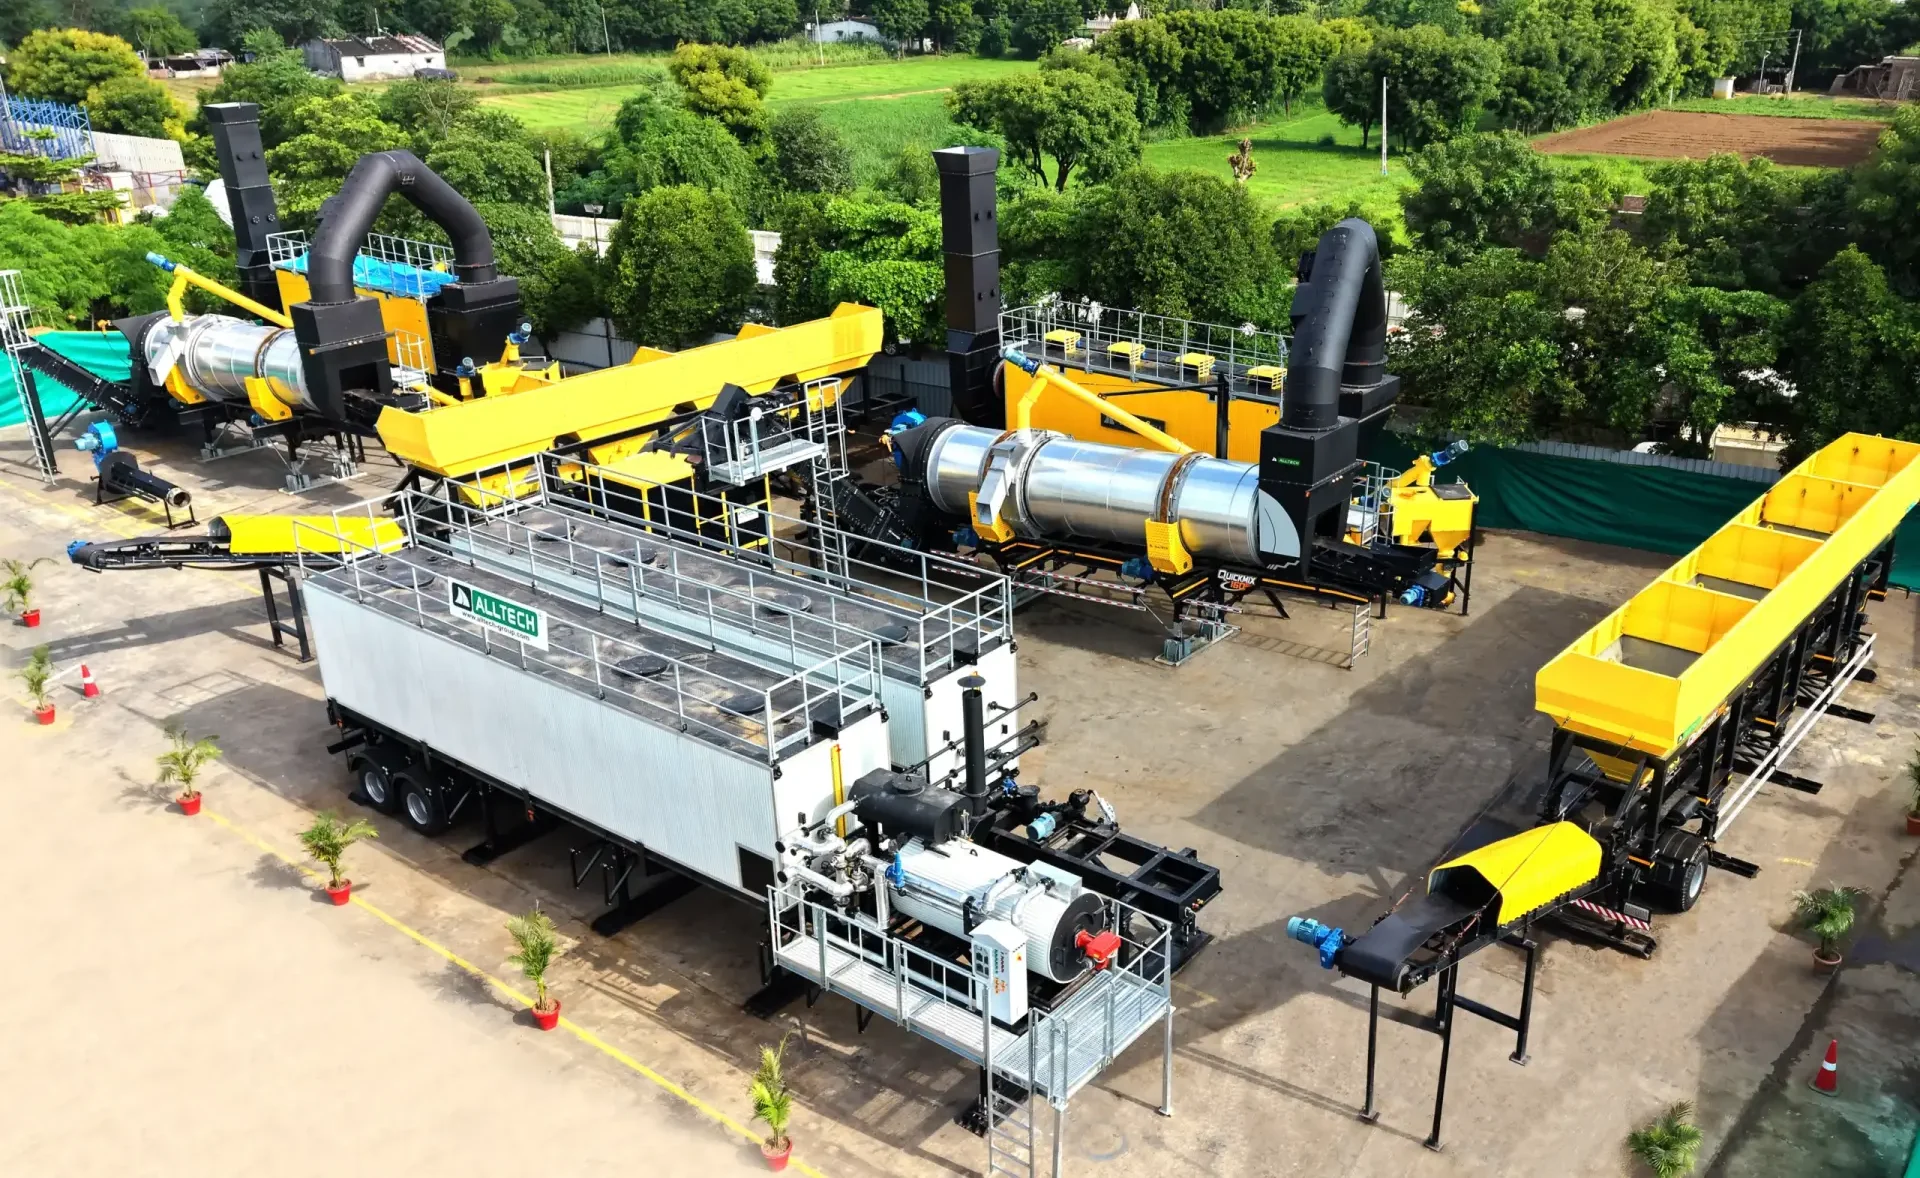
Quickmix: Wheel-Mounted Counter Flow Drum Mix Plant Built to Move With Your Project
Forget the time and cost of building a new plant at every site?
Switch to our QUICKMIX mobile counter flow drum mix plant, with mixing on wheels, up to 30% RAP addition and a bag house filter.
Introduction
Road contractors rarely work in one place. Highway widening, rural road programs and remote quarry-side jobs all need a hot mix close to the work, and the plant has to be moved again when the job ends. A conventional fixed plant is slow and costly to relocate. A mobile plant is designed to be moved, set up and put to work quickly.
The Quickmix series from Alltech is a range of wheel-mounted drum mix plants built on counter flow technology. Capacities run from 90 TPH to 200 TPH, so one family covers small and mid-size contractors as well as high-output highway projects. In this page we explain how the Quickmix works, where it fits, how to choose the right model, and what the market looks like for mobile asphalt plants.
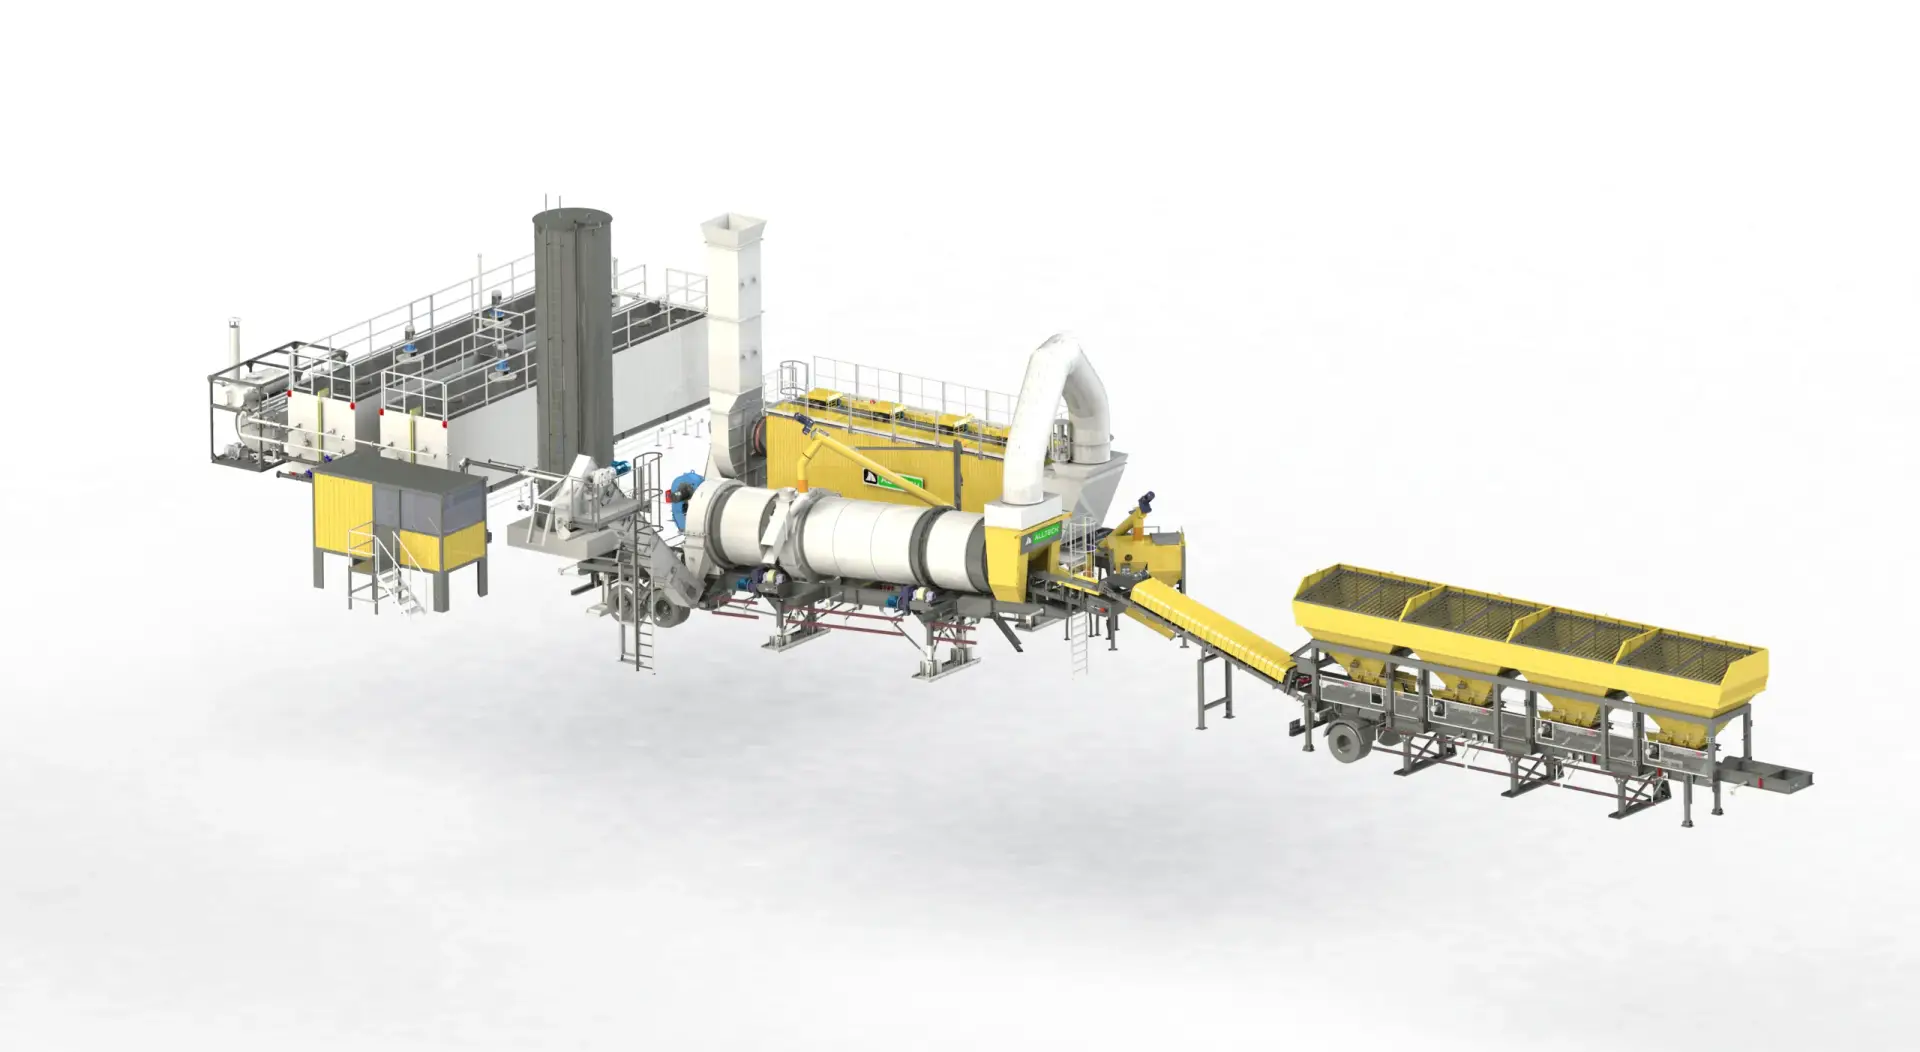
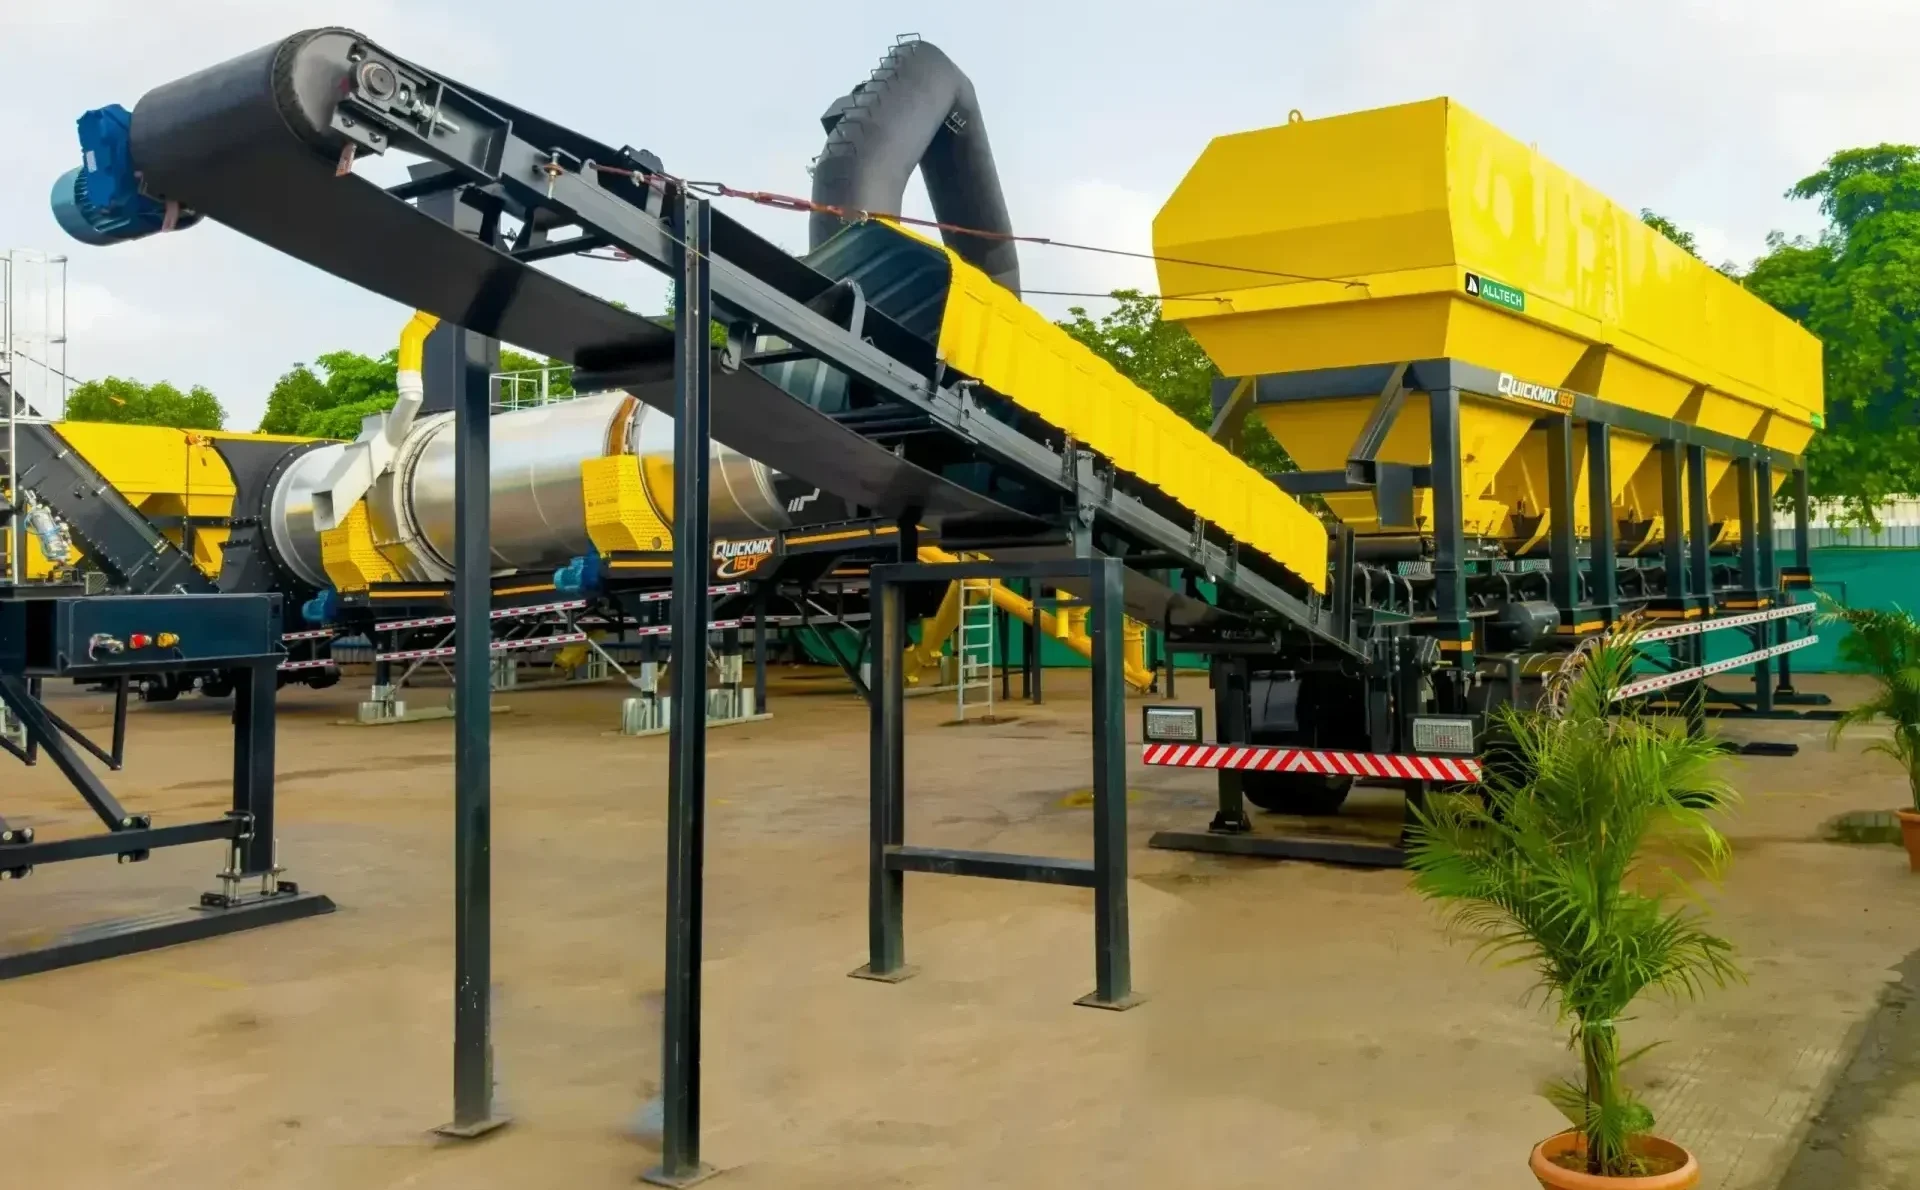
Mobile Cold Feeder Bins
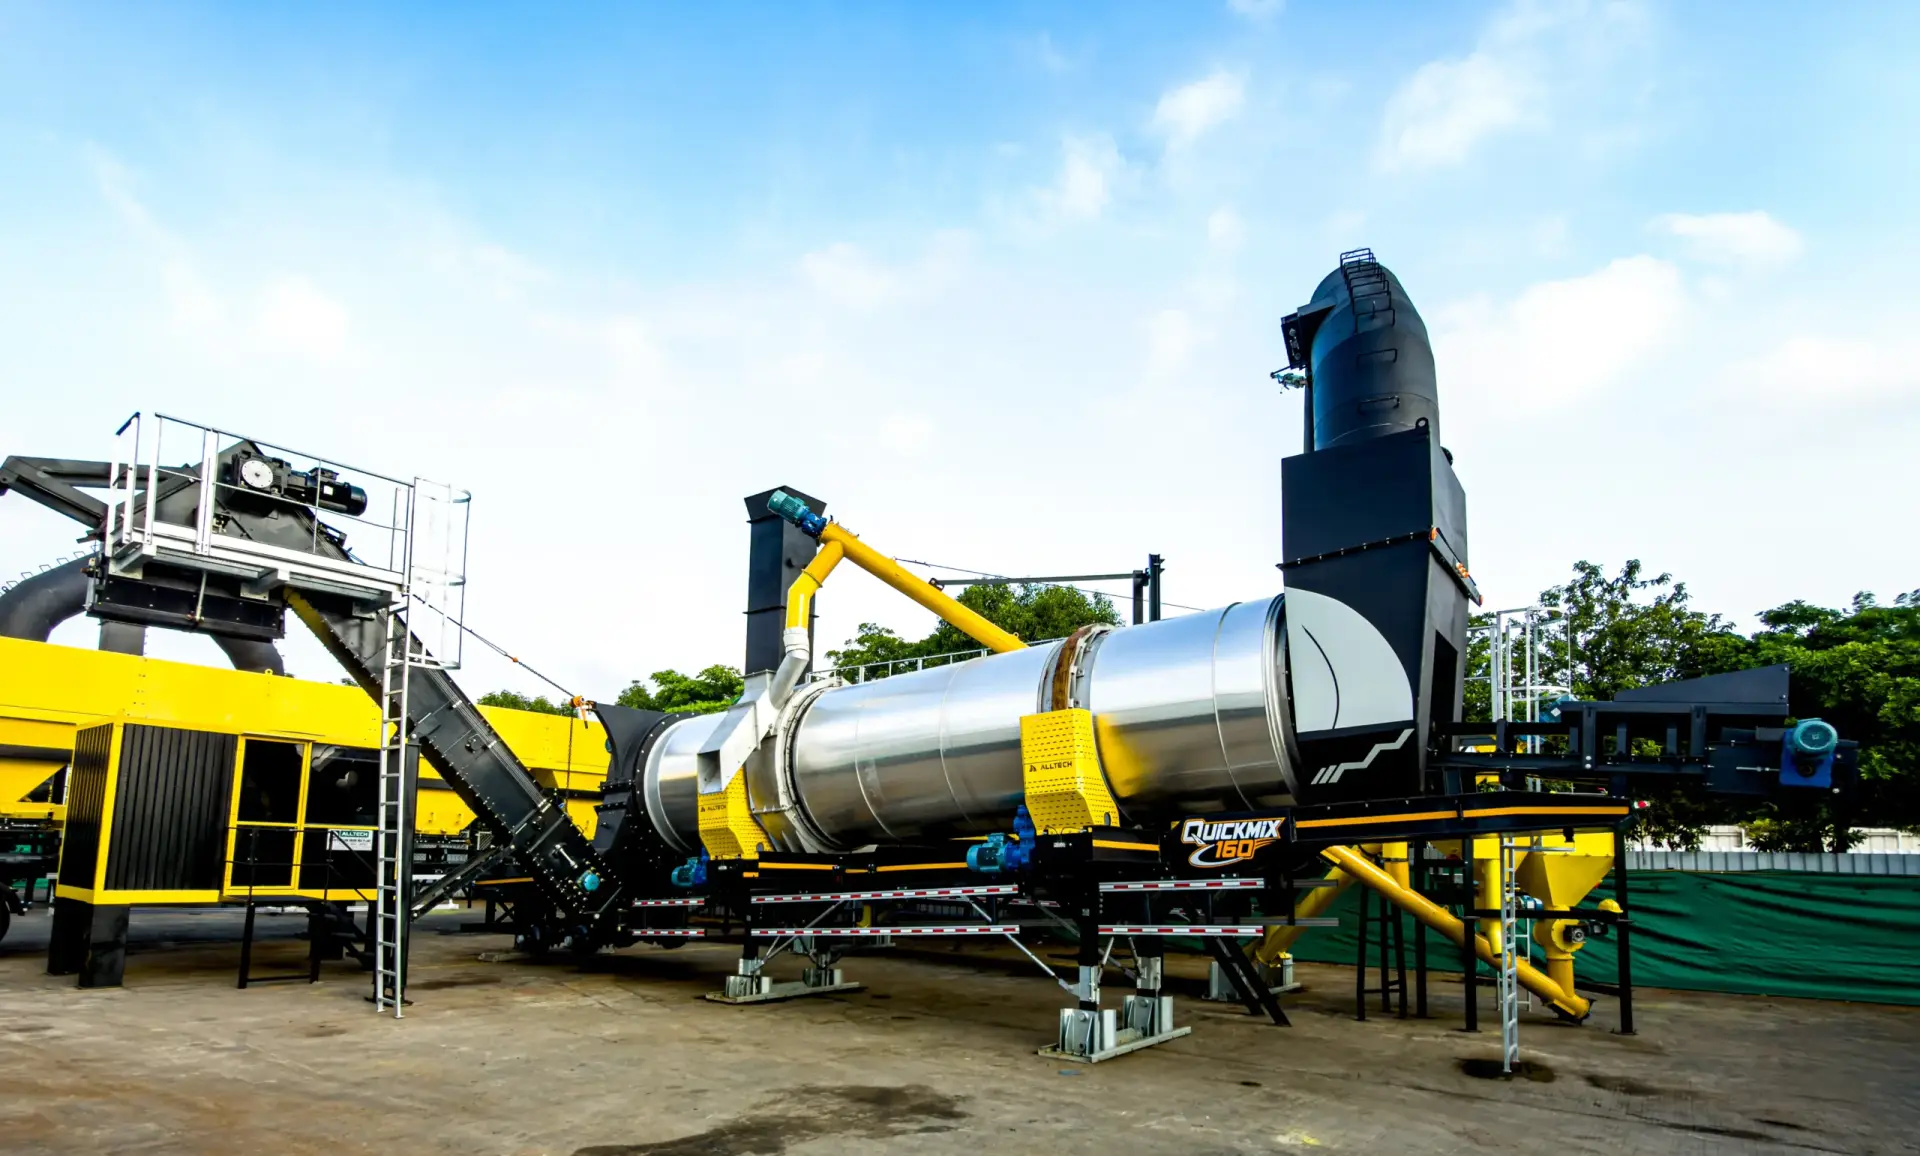
Counter Flow Mobile Dryer Drum
Long Nose Modulating Burner
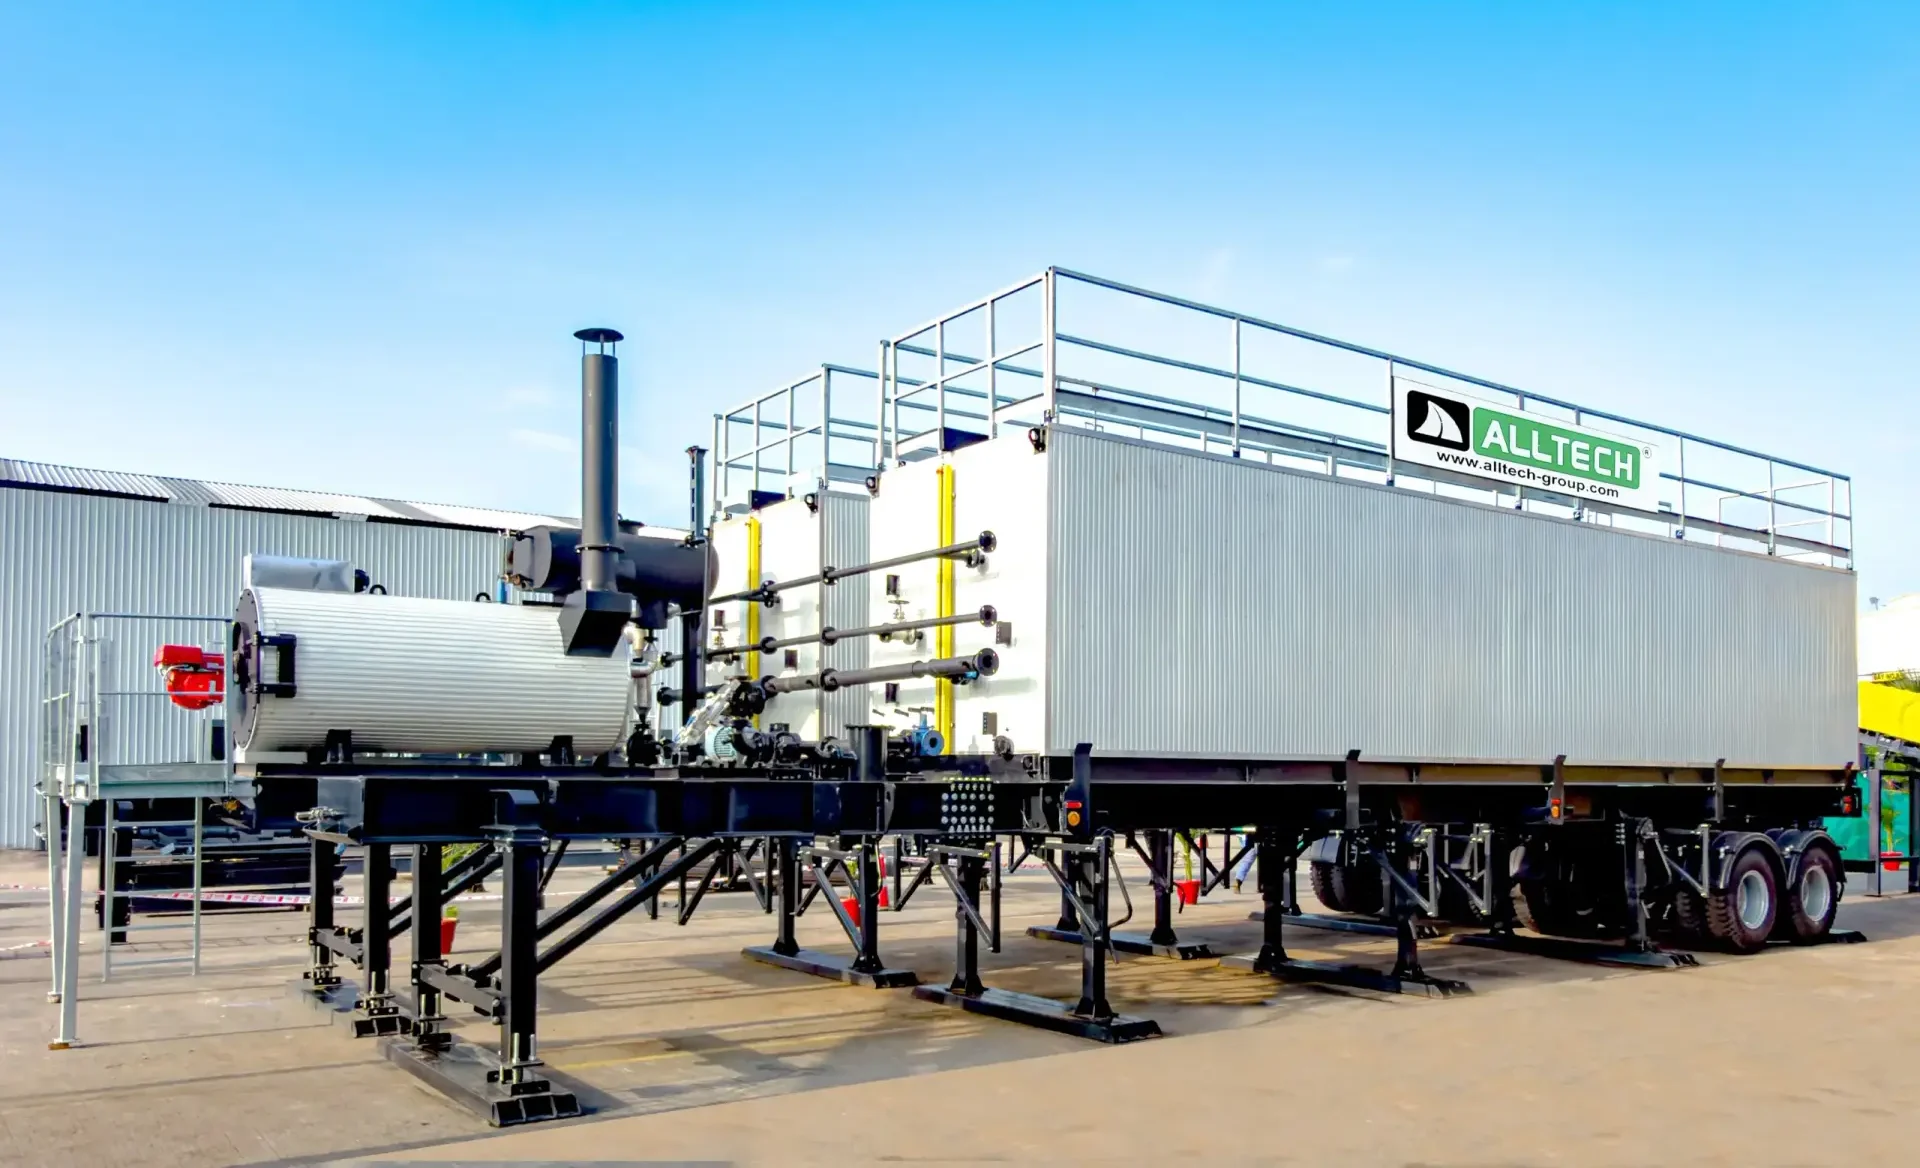
Bitumen Tanks
Control Cabin
Bag House Filter
Thermic Heater
Technical Specification
| PLANT TYPE | Quickmix 90 | Quickmix 120 | Quickmix 160 | Quickmix 200 |
| Plant Capacity @ 3% Moisture | 90 TPH | 120 TPH | 160 TPH | 200 TPH |
| No. of Cold Feeders | 4 | 4/5 | ||
| Cold Feeder Capacity (with Extension Plates) | 8 m³ × 4* | 8.5 m³ × 4/5* | ||
| Dryer Drum Type | Cylindrical, inclined counter-flow type mobile drum | |||
| Drum Size (L × D) | 8 × 1.54 | 9 × 1.8 | 9.5 × 1.8 | 10 × 2.3 |
| Drum Drive | 4W friction drive* | |||
| Modulating Burner Output | 8 MW | 10 MW | 12 MW | 14 MW |
| Burner Type | Long nose modulating burner | |||
| Bag House / Filter System | Pre-separator; bag house filter | |||
| Cleaning Mechanism | Reverse Airflow Type | |||
| LOAD OUT DRAG CONVEYOR (TPH) | ||||
| Recycling Addition | Up to 30% through RAP addition ring | |||
| OPTIONAL ITEMS : | ||||
| BITUMEN TANK | 30/45 MT Horizontal type Direct Heating/ Indirect Heating | |||
| VENTURI TYPE DUST COLLECTING UNIT | ||||
| EXHAUSTER CAPACITY | 22.5 KW | 37.5 KW | ||
| HOT MIX STORAGE SIL | 25-50 MT | |||
| RECYCLING ADDITION | Through RAP addition ring in the drum. | |||
| ADVANTAGE | CONVENTIONAL MOBILE DRUM MIX PLANT | QUICKMIX COUNTER FLOW MOBILE DRUM PLANT | BENEFITS |
| Technology | Older parallel flow design in which heating and mixing happen in the same zone. | Counter flow design in which the heating zone and mixing zone are separate within the same drum. | Bitumen properties and aggregate quality are protected during mixing. |
| Recycled Material | RAP addition is limited or not available. | RAP can be added up to 30% through the RAP addition ring. | Recycled material can be used, which lowers bitumen and aggregate cost. |
| Mobility | Often built as a fixed plant that is later moved. | Wheel-mounted drum designed for relocation between sites. | Faster move between projects and less site preparation. |
| Pollution Control | Venturi type dust collector only, which needs space and water. | Pre-separator and bag house filter with reverse airflow cleaning. | Lower dust emission and easier compliance with local limits. |
| Hot Mix Quality | Quality can suffer because heating and mixing happen together. | Mixing takes place behind the burner flame, away from direct heat. | More homogeneous mix. |
| Burner | Fixed output burner. | Long nose modulating burner (8 to 14 MW across the range). | Output follows demand, which supports fuel savings and low emissions. |
| Fuel Consumption | Higher fuel consumption. | Lower fuel consumption than a conventional drum mix plant. | Lower operating cost per tonne. |
RAP Addition - Efficiency Burner - Mobile on Wheels
Efficient RAP Addition
High Efficiency Burner
Mobile on Wheels
The Quickmix drum allows RAP addition of up to 30% through the RAP addition ring, so contractors can use reclaimed asphalt and reduce virgin material cost.
The drying drum is fitted with a long nose modulating burner of 8 to 14 MW depending on the model, which supports efficient combustion and low emission levels.
The counter flow drum is mounted as a mobile unit. When the job ends, the plant can be moved to the next site instead of being dismantled completely.
What is a Mobile Counter Flow Drum Mix Plant?What is a Mobile Counter Flow Drum Mix Plant?
What is a Mobile Asphalt Plant?
A mobile counter flow drum mix plant is a continuous asphalt plant in which the drying and mixing drum is mounted on a wheeled chassis. Aggregates and exhaust gas move in opposite directions in the drum. Heating happens in one zone and mixing with bitumen happens in a separate zone, so the bitumen is not exposed to direct flame.
How Does a Quickmix Plant Work?
Cold aggregates are loaded into the cold feeders and carried to the drum. Inside the inclined counter flow drum, aggregates travel against the hot gas from the burner and are dried and heated gradually. RAP can be added through the RAP addition ring. In the mixing zone, the heated aggregates are coated with hot bitumen to produce a uniform hot mix. Exhaust gas passes through the pre-separator and the bag house filter, which is cleaned by reverse airflow, before it leaves the stack. The finished mix goes to a storage silo or directly into trucks.
Advantages of Quickmix Plants
Advantages of Counterflow Asphalt Plants
Quick Relocation
The wheel-mounted drum is built to be moved between sites, which reduces idle time between projects.
Energy Efficiency
Counter flow heat transfer and a modulating burner use fuel more efficiently than a conventional drum mix plant.
Recycling Ready
Up to 30% RAP can be added through the RAP addition ring.
Common Applications
Quickmix plants are used in:
- Highway widening and strengthening projects
- Rural and district road programs
- Road maintenance and resurfacing contracts
- Remote and quarry-side projects where a fixed plant is not practical
- Contractors who work on several sites in a year
- Airport, port and industrial area paving
Key Components of a Mobile Counterflow Asphalt Plant
Key Components of a Counterflow Asphalt Plant
All key components of Mobile counterflow asphalt plant such as:
Cold Feeders
Four or five cold feeders (depending on the model) hold different aggregate sizes and feed the drum in the right proportion. Extension plates increase capacity.
Counter Flow Mobile Drum
The cylindrical, inclined drum dries and heats the aggregates and mixes them with bitumen. A four-wheel friction drive turns the drum.
Long Nose Modulating Burner
The burner output changes with plant load, from 8 MW on the Quickmix 90 to 14 MW on the Quickmix 200.
Pre-Separator and Bag House
The pre-separator removes coarse dust first, and the bag house filter collects the fine dust. Reverse airflow cleans the filter bags.
Choosing the Right Counterflow Asphalt Plant
Selecting the right Mobile counterflow asphalt plant depends on various factors such as:
Capacity and Throughput
The plant’s capacity should align with the project’s requirements to ensure timely completion.
Fuel Options
Consider the availability and cost of fuel options, as this will affect operating costs.
Environmental Compliance
Ensure the plant complies with environmental regulation and emission standards.
Supply and Support
Alltech India Limited manufactures road construction equipment in Mehsana, Gujarat, and supplies contractors in India, Africa, the Middle East and other regions. Our engineers support retrofitting, service, spare parts and training.
Conclusion
The Quickmix range brings counter flow quality, RAP addition and bag house emission control to a wheel-mounted plant. With four models from 90 to 200 TPH, it gives contractors a plant that moves with the project without giving up mix quality.
Frequently Asked Questions
The range covers four models from 90 TPH to 200 TPH at 3% aggregate moisture.
Up to 30% RAP can be added through the RAP addition ring in the drum.
In a counter flow plant, aggregates and exhaust gas move in opposite directions, and mixing takes place in a zone separate from the burner flame. This allows RAP addition and a more uniform mix.
Yes. The counter flow dryer drum is a mobile unit mounted for transport between sites.
- A long nose modulating burner with an output from 8 MW (Quickmix 90) to 14 MW (Quickmix 200).
A pre-separator and a bag house filter with reverse airflow cleaning are standard. A venturi type dust collecting unit is optional.
Yes. A 30 MT horizontal bitumen tank (direct or indirect heating) and a 25-50 MT hot mix storage silo are available as options.
Choose by the hourly output you need at your site’s aggregate moisture. Contact us with your project details and we will recommend a model.
Yes, manufacturers often offer customization options to meet project-specific needs.
Yes. Alltech supports commissioning, operator training, spare parts and service.